Leave Your Message
Choosing an Industrial Ultrasonic Welder is a production decision, not a catalog exercise. The wrong setup can leave weak joints, visible marks, or inconsistent results across a shift. In its 2024 market analysis, Grand View Research estimated the global ultrasonic welding market at approximately US$1.1 billion in 2023 and projected continued growth through 2030. That signals rising interest, but it does not prove every application suits ultrasonic welding. Material, joint geometry, and production rate still matter.
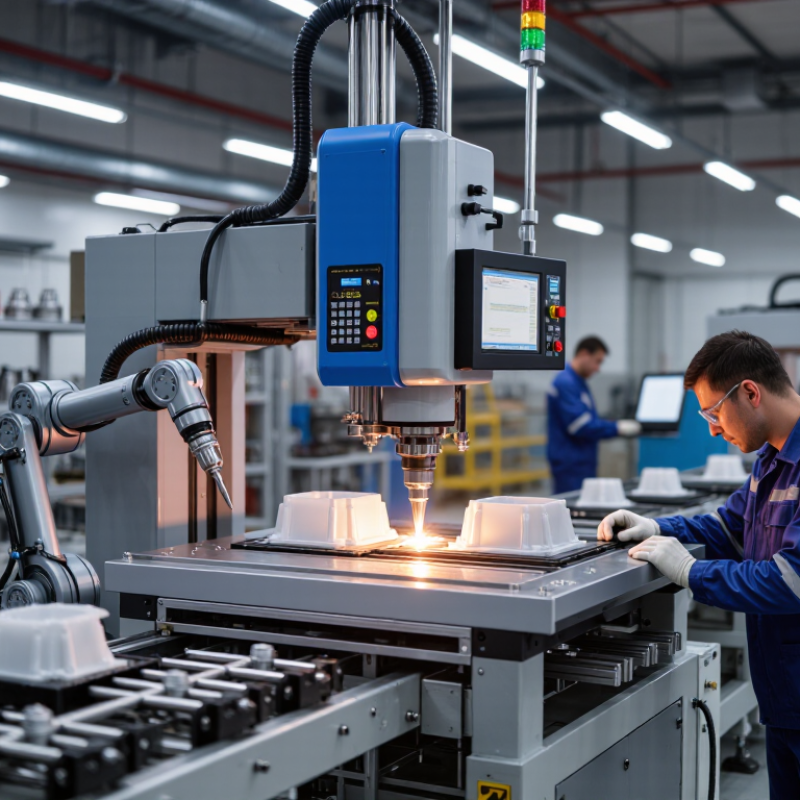
Automation adds another practical consideration. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023 in its World Robotics 2024 report. A welder may need to work beside robots, conveyors, or operators, so controls, cycle timing, and maintenance access deserve close attention. Small details count. A narrow fixture opening can complicate part loading. A horn that is difficult to replace can slow routine service. These are easy to overlook during a first demonstration.
The following seven tips focus on choices buyers can verify: material compatibility, required joint strength, frequency and power, tooling, process controls, integration, and supplier support. Ask vendors to test your actual parts, not just similar samples. Record weld time, appearance, and strength. Then review the results with production and quality teams. One caution: a promising sample is not a production guarantee. Real output may vary, and that uncertainty should shape the purchase decision.
7 Tips for Choosing an Industrial Ultrasonic Welder
Define the workpiece before comparing machine specifications. Record its length, thickness, mass, surface finish, and dimensional tolerance. A thin molded part may need controlled amplitude, while a larger housing may require higher energy and clamp force. The American Welding Society projects a U.S. shortage of about 330,000 welding professionals by 2028. That makes repeatable setup more important than operator intuition.
Identify the material pair next. Similar thermoplastics usually weld more predictably than incompatible polymers. Reinforcement, moisture, pigments, and recycled content can change melt behavior. Test the actual production resin, not only a supplier datasheet sample. I have seen teams compare power first. That shortcut fails.
Joint geometry decides whether the vibration reaches the intended interface. Inspect the energy director, wall thickness, weld depth, and part alignment. A small mismatch can create flash, weak spots, or cosmetic marks. The joint should guide energy, not absorb it. Match the horn face and anvil to the part’s shape, then review frequency, amplitude, pressure, trigger force, and cycle limits. Industry quality studies consistently emphasize process capability and traceability; record these settings during trials. Leave room for adjustment. Real parts vary. Their variation may expose an assumption you missed. Compare welders only after these measurements are documented, using destructive tests and repeatability data from several production-representative batches.
| Tip | Define Before Comparing | Why It Matters | What to Check | Example Details to Record |
|---|---|---|---|---|
| 1 | Workpiece and part features | Part size, mass, wall thickness, ribs, and nearby features affect how the part can be supported and how vibration reaches the joint. | Confirm the part can be located repeatably and supported close to the weld without obstructing the tooling. | Overall dimensions, part mass, wall thickness, rigid features, and cosmetic surfaces. |
| 2 | Material pair and grade | Thermoplastics generally need compatible melting behavior and intimate contact at the interface. Fillers, additives, moisture, and grade differences can change weld response. | Identify each resin and grade, including reinforcement or additives; validate dissimilar-material combinations with weld trials. | Resin family, grade, glass-fiber content, colorant or additive, and whether the materials are identical or dissimilar. |
| 3 | Joint geometry | Joint design influences energy concentration, alignment, flash, and the consistency of the interface during collapse. | Review the joint drawing and tolerances. Common thermoplastic joint designs include energy directors and shear joints, subject to part and material suitability. | Joint type, weld length or perimeter, energy-director dimensions, overlap, gaps, and allowable flash. |
| 4 | Required weld performance | The acceptance target determines how the process should be developed and which measurements or tests must be available. | Specify strength, leak-tightness, appearance, dimensional limits, and any applicable qualification or validation tests. | Minimum pull or burst result, leak requirement, maximum flash, and inspection method. |
| 5 | Tooling and part support | A well-matched horn and fixture help deliver vibration to the joint while limiting unwanted movement or damage to the part. | Assess access, contact area, fixture stiffness, part location, and clearance for the horn and any nest features. | Horn contact surface, fixture concept, loading direction, locating datums, and tooling changeover needs. |
| 6 | Production rate and automation | Cycle time, operator handling, and integration requirements affect the press configuration, controls, and material-flow design. | Separate weld time from total station cycle time; include loading, unloading, inspection, and any automated handling. | Target parts per hour, shifts per day, manual or automated loading, and available floor space. |
| 7 | Process control and validation | Monitoring and repeatable setup help detect process variation, but the appropriate controls depend on the application and quality plan. | Compare available control modes, parameter logging, alarms, recipe management, and data export against documented process needs. | Required records, process limits, traceability level, sample plan, and revalidation criteria. |